








- Gravity Roller Conveyors
- Driven Roller Conveyors
- Casflex Conveyors
- Extendable Conveyors
- Scale Conveyor
- Fruit Sorting Conveyor
- Pallet Handling Conveyors
- Turn Tables
- Belt Conveyors
- Aluminum Conveyors
- Inter-floor Conveyors
- Builders or Construction Conveyors
- Truck Loader Conveyors
- Single Boom Stackers
- Bottling Conveyor
- Lift Tables
- Roller Tracks
- Parts and Accessories
- Turnkey Projects


Gravity Roller Conveyors
Gravity roller conveyors provide a simple, reliable and cost-effective solution for moving products with minimal maintenance. Their robust design makes them ideal for warehouses, distribution centres, production lines and assembly areas.
As these conveyors require no motor or electrical power, products are moved manually or by gravity when the conveyor is installed on a slight incline. This makes them an economical and energy-efficient choice for a wide range of applications.
Convey Systems manufactures gravity roller conveyors using high-quality components and offers rollers in a variety of materials, including:
– Mild Steel (Natural Finish)
– Zinc Plated (Galvanised)
– Stainless Steel
– Aluminium
– Plastic
Our standard roller load capacities range from 20 kg to 450 kg per roller, ensuring the correct solution for light, medium and heavy-duty applications.
Standard Roller Diameters
– 25 mm
– 38 mm
– 50 mm
– 60 mm
– 63 mm
– 76 mm
– 89 mm
For products requiring extra protection, we also offer PVC-coated rollers. These are ideal for delicate or finished products where scratches, marks or surface damage must be avoided.
Whether you require a simple carton handling system or a heavy-duty material handling solution, our gravity roller conveyors can be custom manufactured to suit your exact application.
This version is more sales-oriented, improves SEO with terms like material handling, warehouses, distribution centres, and *custom manufactured*, and ends with a stronger call to action without sounding overly promotional.
Driven Roller Conveyors
We offer both line shaft and chain driven roller conveyors.
Line shaft conveyors
- Powered via a shaft
- Suitable for lighter applications up to 100kg per meter
- There are a series of plastic spools with one spool for each roller
- Poly-urethane drive bands run from the spool to each roller
- Drive bands acts as the connection between the spool and the roller; making the rollers rotate
- Rotation of the rollers then pushes the product along the conveyor
- Shaft is driven via a close coupled shaft mounted motor and gearbox
- Controlled by a variable speed drive or PLC
Applications & Advantages
- Where accumulation of the product is required
- Drive spools are free running on the drive shaft and therefore can be stopped, while the shaft continues to rotate, if a certain amount of resistance is applied
- It is quiet in operation
- Reliable
- Easy to install
- Low maintenance
- Low cost
- Can be adapted to take bends, lane mergers and even turntables.
Chain driven conveyors
- Driven by separate loops of chain
- Running on dual sprockets or a continuous chain that is in contact tangentially to all the roller sprockets
- Depending on the type and function of the conveyor either double or single sprockets are fitted to the roller
Applications & Advantages
- Simple, efficient, rugged, and relaible design
- Ideal for transporting pallets, containers, drums, and boxes
- Modular design offers the ability to have controllable drive zones for zero back pressure, accumulation zones, indexing, mergers and simple insertion of turntables and pop-ups
- PVC coated rollers can also be supplied, these are used for delicate products that cannot be scratched.
Standard roller sizes: 38mm, 50mm, 60mm, 76mm and 89mm


Casflex Expandable Conveyors
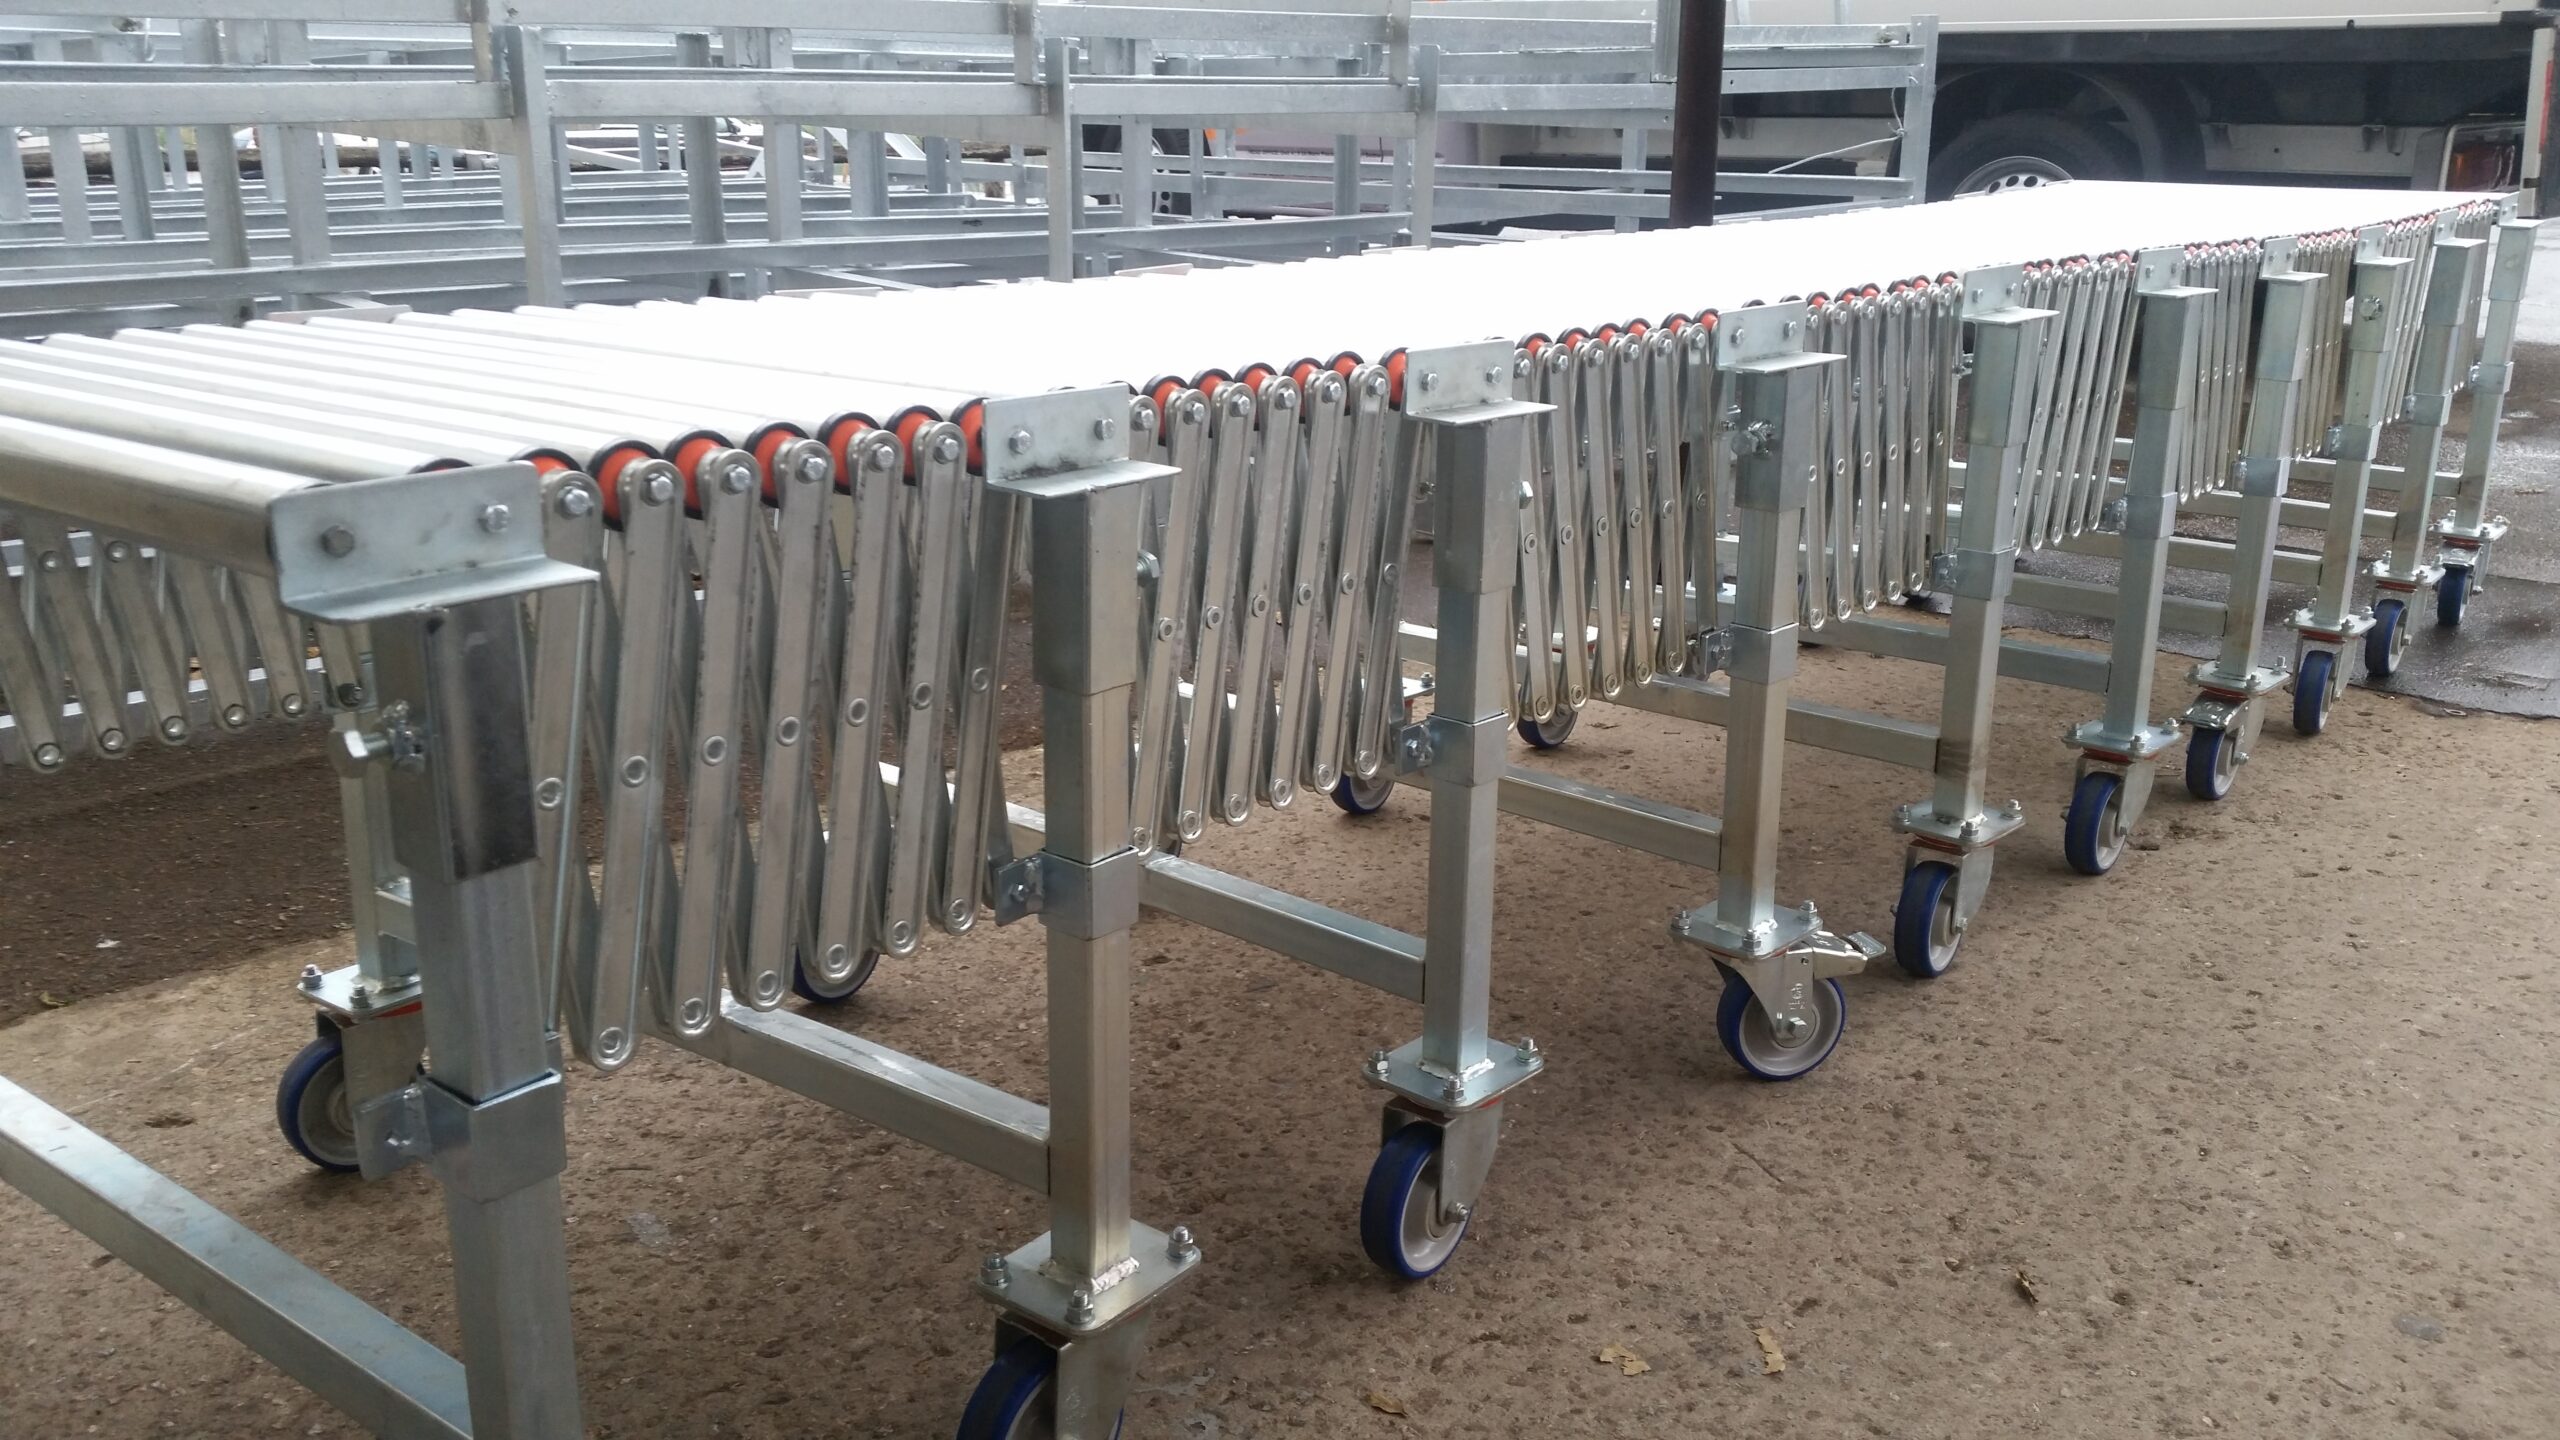
Casflex expandable conveyors provide a flexible, space-saving solution for loading, unloading and transporting cartons, boxes, totes and lightweight products. Their unique expandable design allows the conveyor to extend when required and retract into a compact footprint when not in use, making them ideal for warehouses, distribution centers, courier depots and packing facilities where floor space is at a premium.
Manufactured using a heavy-duty scissor-link framework, each conveyor module extends from 1,000 mm to 3,000 mm, allowing a single conveyor to cover varying distances with ease. Multiple modules can also be joined together to create longer conveyor systems, providing maximum flexibility as your operation grows.
Fitted with lockable swivel castors, Casflex conveyors can be quickly moved into position, extended to the required length and securely locked in place. Their flexible design also allows the conveyor to negotiate corners, curve around obstacles and accommodate uneven floor levels, making them a versatile solution where fixed conveyors are not practical.
These conveyors are ideal for conveying cartons, boxes, plastic totes, parcels, bins and other lightweight packaged products in industries such as warehousing, logistics, courier services, e-commerce fulfilment, manufacturing and distribution.
Standard Specifications
- Collapsed Length: 1,000 mm per module
- Extended Length: 3,000 mm per module
- Roller Diameter: 50 mm
- Load Capacity: Up to 50 kg per meter
- Conveyor Widths: 300 mm to 700 mm
- Adjustable Working Height: 300 mm to 900 mm
Features
- Extendable and retractable design saves valuable floor space
- Modular construction allows multiple sections to be connected together
- Lockable swivel castors for easy movement and positioning
- Flexible enough to negotiate bends, corners and uneven floor surfaces
- Quick to deploy with no permanent installation required
- Low maintenance and virtually maintenance-free operation
- Robust steel construction for long service life
- Custom sizes and configurations available
Whether you’re loading delivery vehicles, unloading containers, creating temporary packing lines or moving products through a warehouse, Convey Systems’ Casflex expandable conveyors provide a practical, reliable and highly adaptable material handling solution that improves efficiency while maximizing available workspace.


Extendable Conveyors
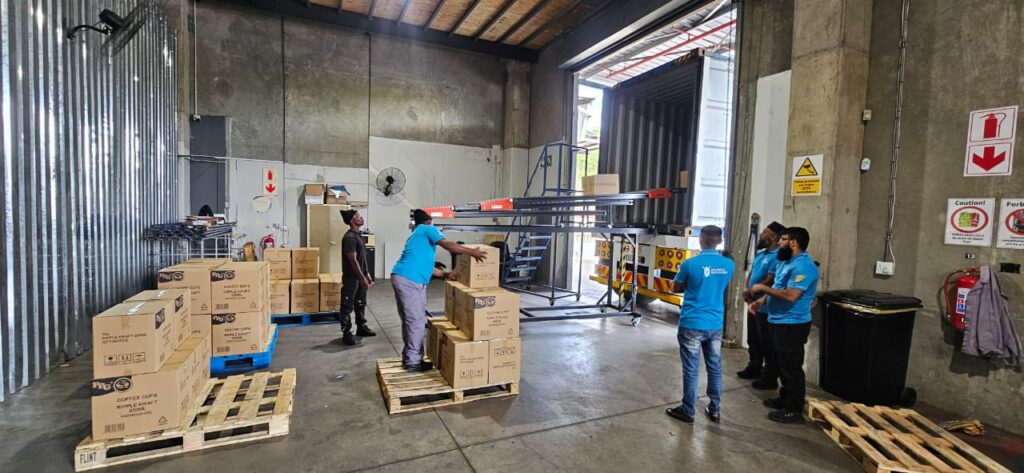
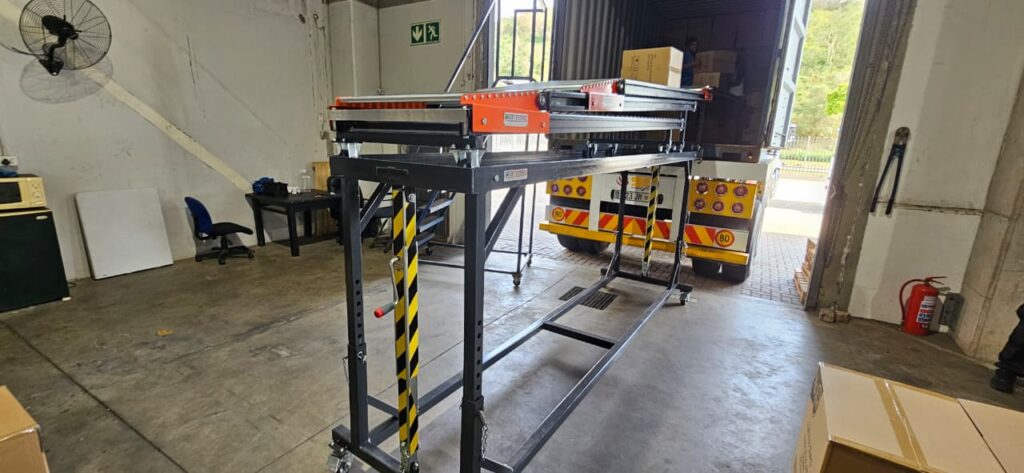
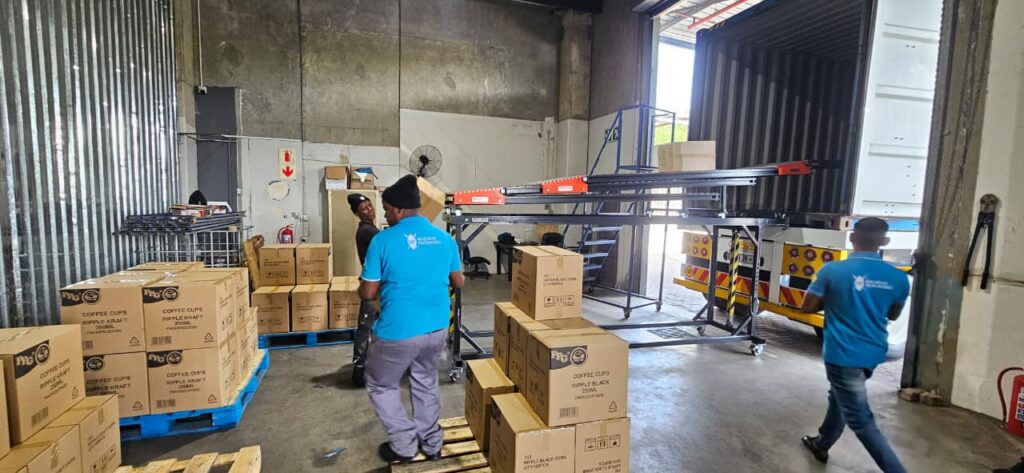
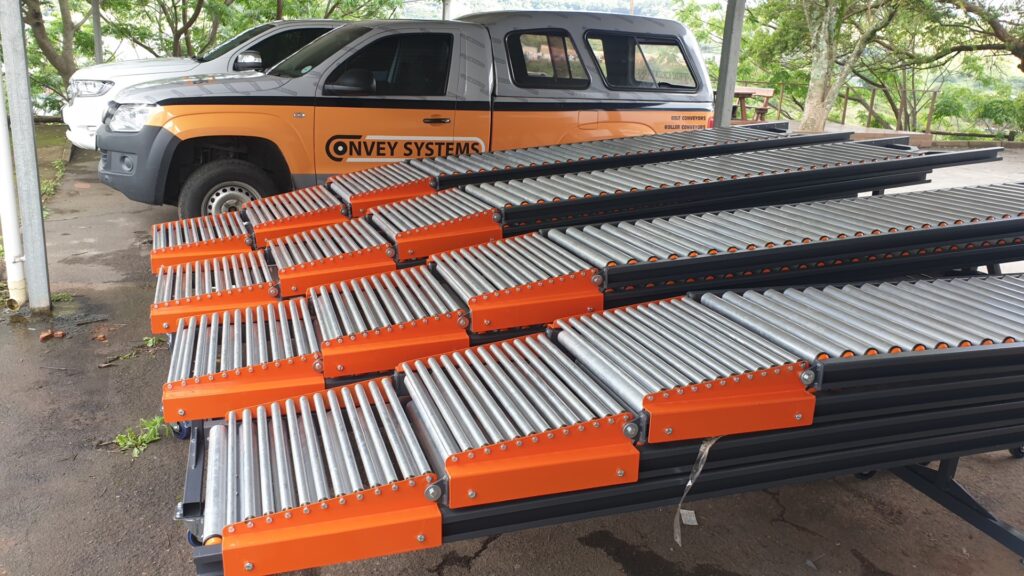
Convey Systems’ extendable conveyors provide a flexible, space-saving solution for loading, unloading and transporting cartons, boxes, totes and other lightweight products. Designed for operations where conveyor lengths need to change regularly, these conveyors can be extended when required and retracted into a compact footprint when not in use, making them ideal for warehouses, distribution centres, courier depots and e-commerce fulfilment centres.
Manufactured using a robust scissor-link framework, our extendable conveyors provide outstanding flexibility while maintaining smooth, reliable product flow. The modular design allows the conveyor to adapt to different loading distances, making it the perfect solution for truck loading, container unloading, order fulfilment, sorting lines and temporary production areas.
Every support leg is fitted with heavy-duty lockable swivel castors, allowing the conveyor to be easily repositioned and securely locked into place. The flexible design also enables the conveyor to negotiate gentle bends, uneven floor levels and confined spaces where fixed conveyor systems are not practical.
Our extendable conveyors are widely used throughout the logistics, warehousing, courier, manufacturing, packaging and distribution industries for handling cartons, parcels, plastic totes, bins, boxes and other packaged products.
Standard Specifications
- Minimum Length: 4,600 mm
- Maximum Extended Length: 11,800 mm
- Roller Diameter: 50 mm
- Maximum Load Capacity: 50 kg per metre
- Standard Width: 600 mm
- Adjustable Working Height: 900 mm to 1,400 mm
Features
The extendable design allows the conveyor to be quickly lengthened or shortened to suit changing operational requirements, while its compact retracted size saves valuable storage space when not in use. Heavy-duty lockable swivel castors provide excellent mobility, allowing a single conveyor to be easily moved between loading bays or workstations.
Designed for reliability and long service life, the conveyor features a robust steel construction capable of withstanding demanding industrial environments. Its flexible design makes it ideal for long conveying distances, temporary production lines, loading docks and areas where permanent conveyor installations are not practical.
Whether you’re loading trucks, unloading shipping containers, sorting parcels or transporting cartons through a warehouse, Convey Systems’ extendable conveyors provide a versatile, efficient and cost-effective material handling solution that increases productivity while maximising valuable floor space.

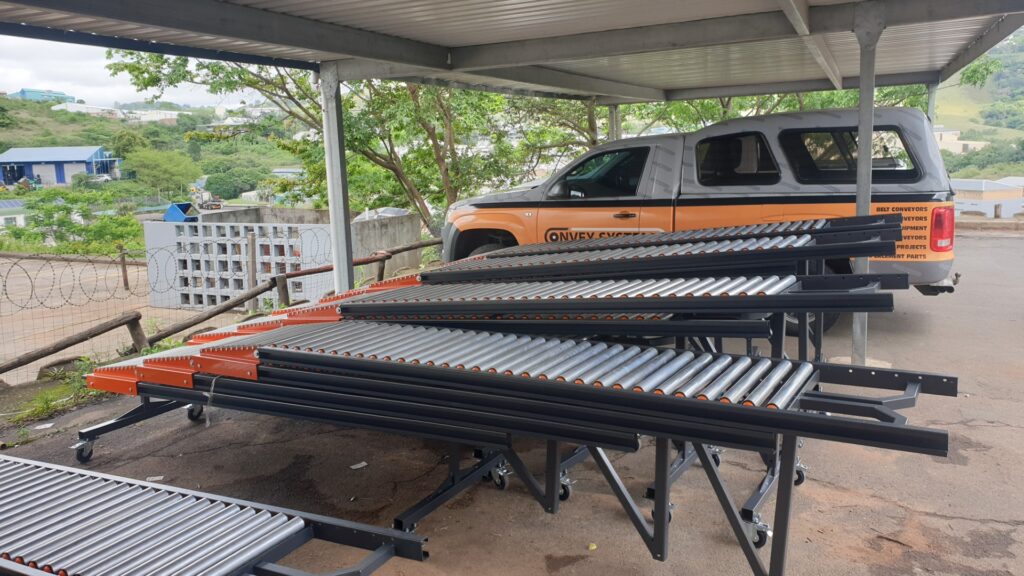
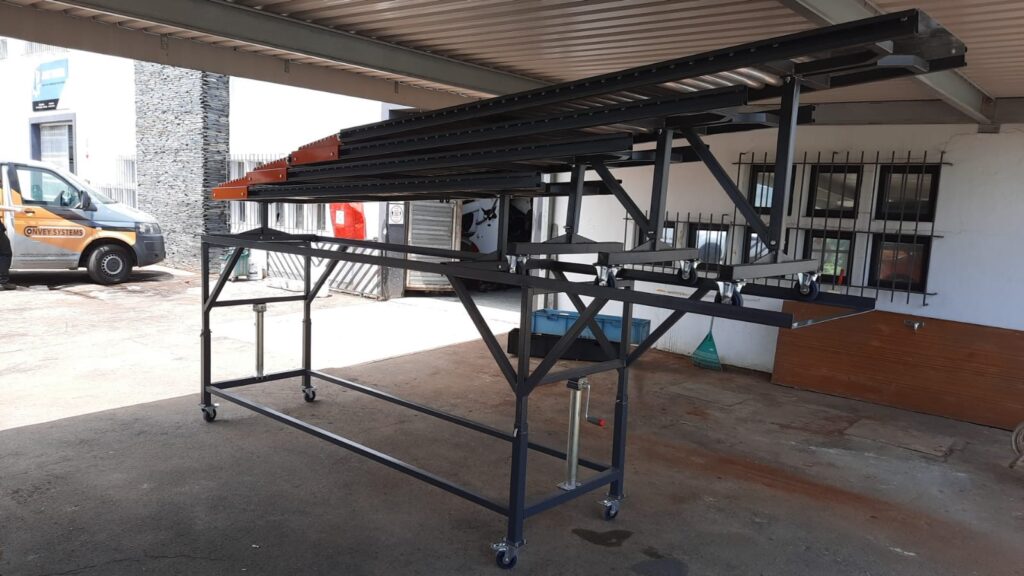
Scale Conveyors
Streamline Your Weighing and Handling Process
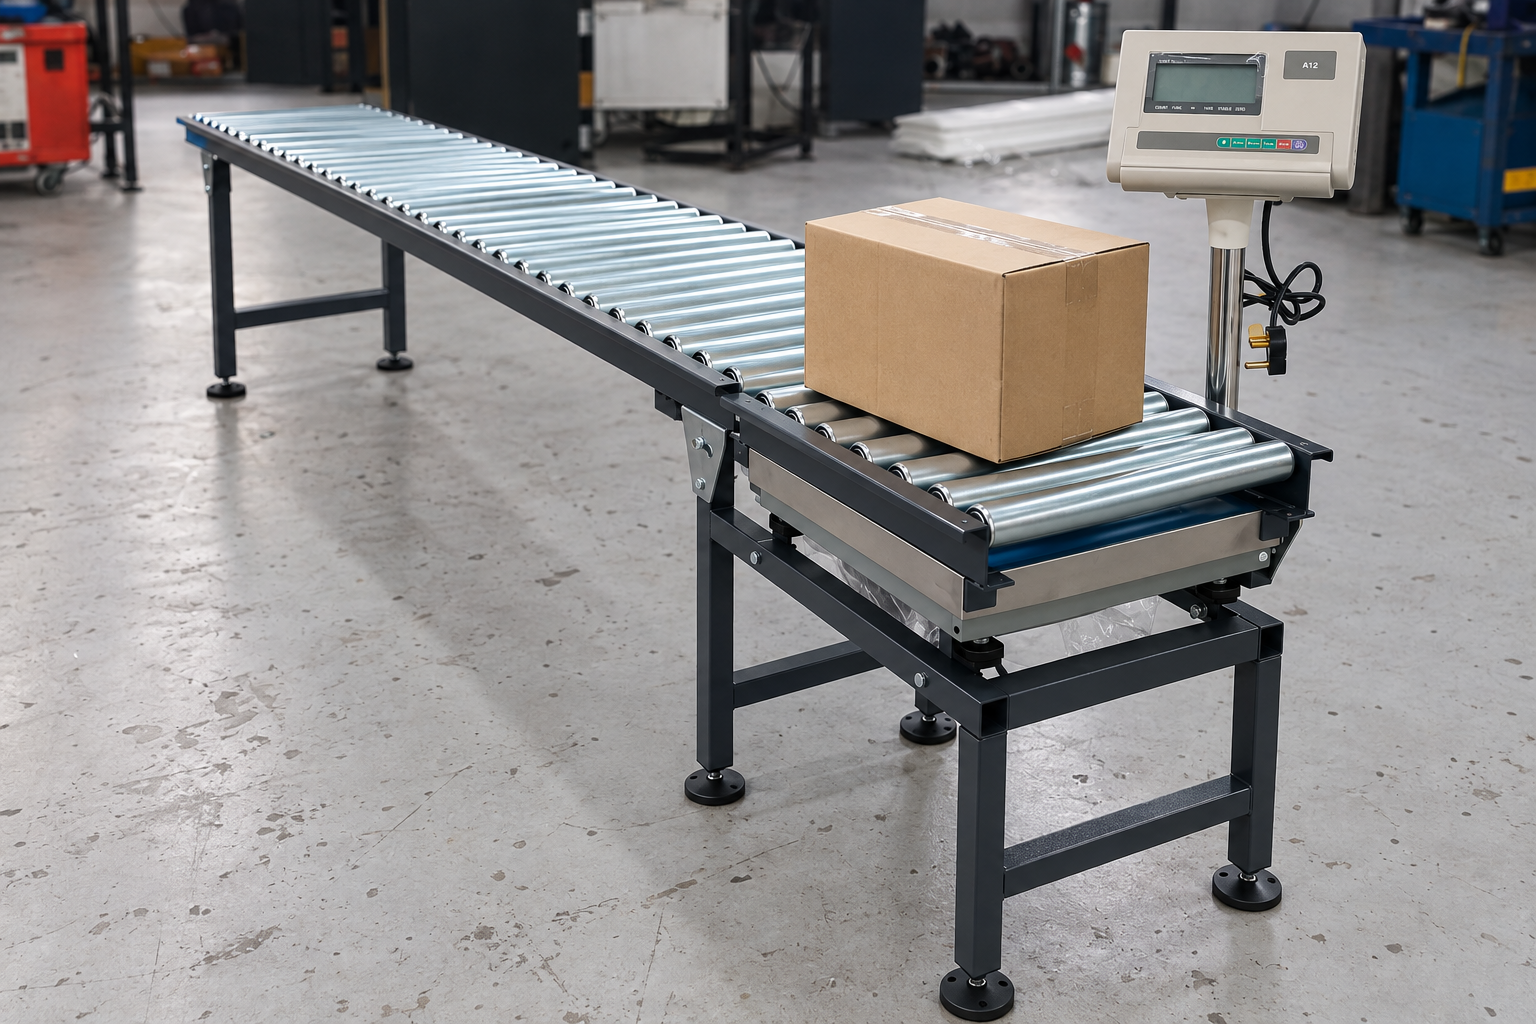
Our Scale Conveyors combine precision weighing with efficient material handling, enabling real-time weight monitoring and automated sorting or batching during product flow. Designed for high accuracy and durability, these conveyors help industries optimise throughput while maintaining product consistency and traceability.
Perfect for use in packing lines, grading systems, and quality control stations, our scale conveyors are tailored to meet demanding production environments.
Key Features:
⚖️ Integrated High-Precision Weighing
Built-in load cells provide accurate, real-time weight data for bags, boxes, or loose products in motion.
🚀 Inline Weighing Without Interruption
No need to stop the line—our dynamic weighing technology ensures seamless operation without bottlenecks.
📊 Smart Display and Control Interface
User-friendly control panels with weight display, tare, zeroing, and data export functions. Optional integration with PLC and ERP systems.
🛠️ Stainless Steel or Powder-Coated Options
Hygienic and robust construction suitable for both food-grade and industrial applications.
🔧 Custom Sizing & Capacity Ranges
Available in various belt widths, lengths, and weight ranges—from 5kg up to 100kg and beyond.
📥 Optional Features
Automatic rejecters, weight batching logic, barcode/RFID integration, and reporting software.
Applications:
Agriculture: Inline weighing of bags of grain, seeds, and fertilizer
Food Industry: Portion control and batch weighing for packaged or unpackaged food items
Manufacturing: Weight verification of components, cartons, or finished goods
Logistics: Check-weighing for parcels, freight, and cargo before dispatch
Benefits:
✅ Improved Accuracy – Reduce product giveaway and ensure compliance with weight regulations
✅ Increased Throughput – Weigh while conveying to avoid downtime or stoppages
✅ Cost-Effective – Optimise raw material use and streamline packaging
✅ Data-Driven – Collect and analyse weight data for traceability and inventory control
✅ Customizable – Fully adaptable to your facility layout and output needs
Reliable Weighing Solutions from Start to Finish
Whether you’re upgrading your line or building a new system, we provide turnkey scale conveyor systems designed to deliver reliability, speed, and precision.
Bag Stackers


Fruit Sorting Conveyors
Convey Systems designs and manufactures high-quality fruit sorting conveyors for the fresh produce industry. Our conveyor systems are engineered to transport, inspect, grade, sort and pack fruit and vegetables while minimising bruising, product damage and waste. Designed for continuous operation, our conveyors improve productivity, maximise throughput and maintain the highest standards of product quality.
Our fruit handling systems are suitable for a wide range of fresh produce, including:
- Citrus (oranges, lemons, limes, naartjies and grapefruit)
- Mangoes
- Bananas
- Apples
- Pears
- Avocados
- Tomatoes
- Potatoes
- Onions
- Peppers
- Cucumbers
- Pumpkins
- Butternut
- Kiwifruit
- Peaches
- Plums
- Nectarines
- Apricots
- Pomegranates
- Grapes
- Blueberries
- Strawberries
- Raspberries
- Cherries
- Pineapples
- Pawpaw (Papaya)
- Guavas
- Litchis
- Macadamia Nuts
- Pecan Nuts
- Walnuts
- Almonds
- Chestnuts
- Coffee Beans
- Cocoa Beans
- Other fresh produce and agricultural products
Every conveyor is custom designed to suit your product, production capacity and facility layout. Systems are available in food-grade stainless steel or aluminium construction, making them ideal for packhouses, food processing facilities and agricultural operations where hygiene and corrosion resistance are essential.
Features
- Gentle product handling to minimise bruising
- Food-grade conveyor belts and components
- Stainless steel or aluminium construction
- Hygienic, easy-to-clean design
- Variable speed drive options
- Modular design for future expansion
- Low maintenance and reliable operation
- Custom-built to suit your production line
Complete Packing Line Integration
Our fruit sorting conveyors can be integrated with a wide range of processing and packing equipment, including:
- Fruit washing systems
- Drying conveyors
- Roller inspection tables
- Manual sorting stations
- Automatic grading systems
- Size grading equipment
- Colour sorting systems
- Optical vision inspection
- Weighing systems
- Packing tables
- Box and crate filling stations
- Reject conveyors
- Metal detectors
- Labelling systems
- Barcode scanners
- Inkjet printers
- PLC control systems and automation
Whether you’re packing citrus, mangoes, bananas, tomatoes, apples, avocados, macadamia nuts or any other fresh produce, Convey Systems can design a complete turnkey conveyor solution that increases productivity, improves product quality and reduces labour costs. From small packhouses to large commercial fruit processing facilities, our conveyor systems are built for reliable, long-term performance.


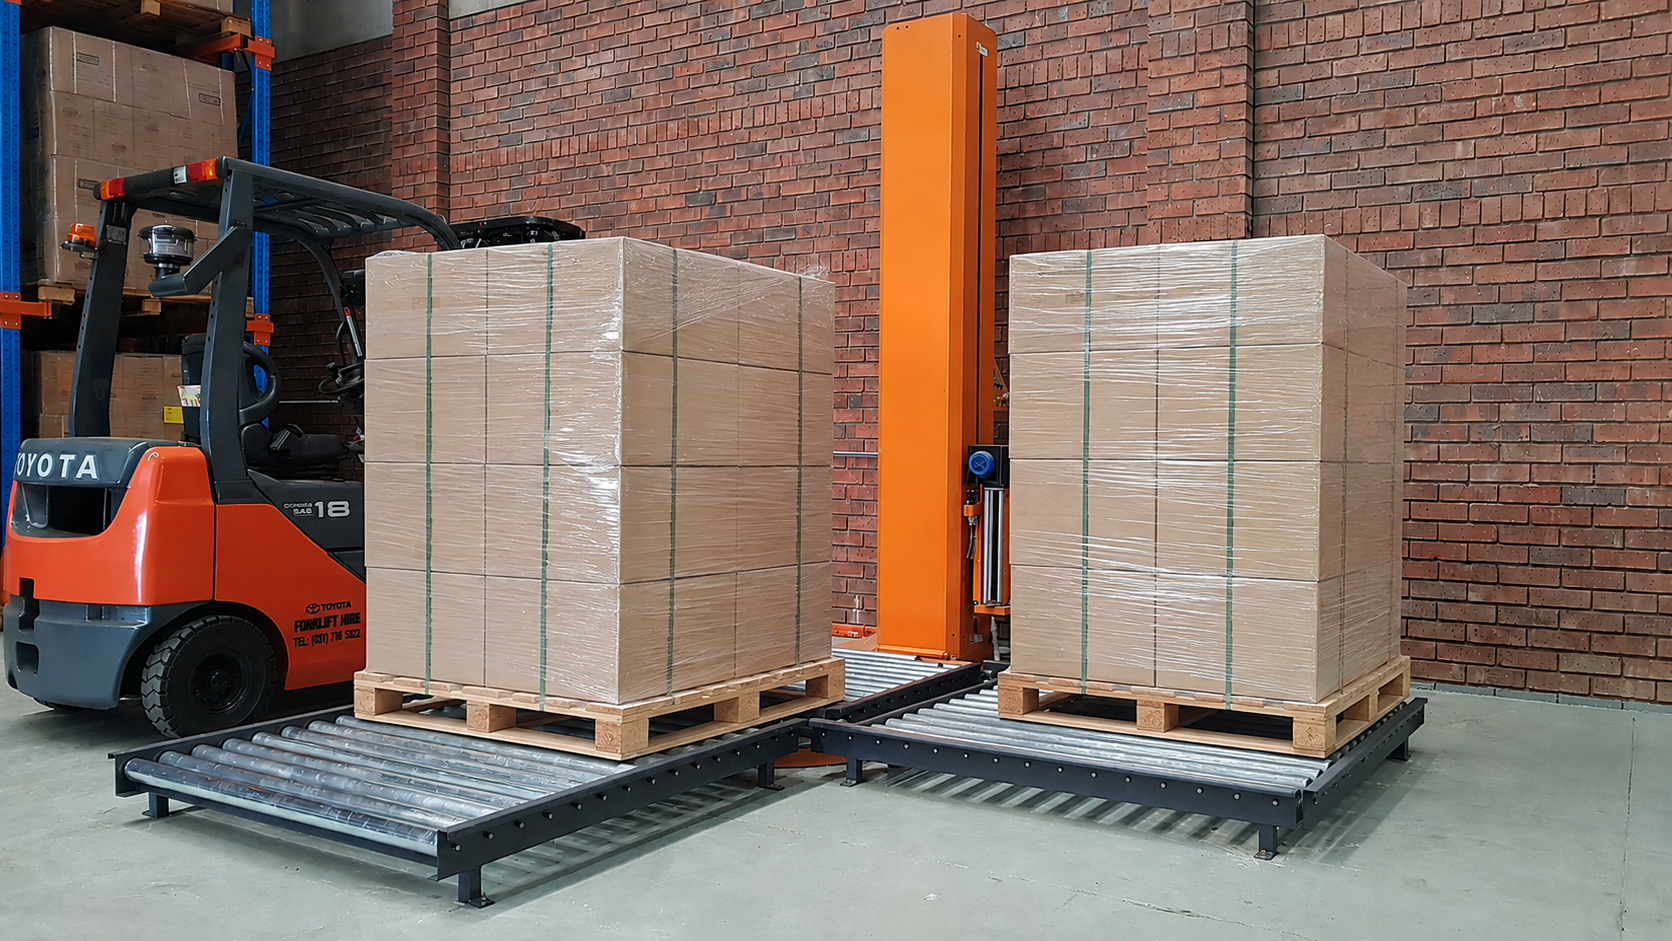
Pallet Handling Conveyors
Pallet handling conveyors are designed to move heavy palletised loads safely, efficiently and reliably throughout manufacturing plants, warehouses and distribution centres. Built for demanding industrial environments, these systems improve productivity, reduce manual handling and streamline the movement of goods between workstations, storage areas and dispatch zones.
At Convey Systems, every pallet handling conveyor is custom designed and manufactured to suit your pallet size, load capacity and production requirements. Whether you require a simple straight conveyor or a fully automated pallet handling system, we provide robust solutions engineered for long-term performance.
Our pallet handling systems can accommodate a wide range of pallet sizes and load capacities, making them suitable for industries including manufacturing, food and beverage, logistics, packaging and warehousing.
Features
- Heavy-duty industrial construction
- Custom-built to suit your pallet size and load
- Roller and chain conveyor options available
- Suitable for wooden, plastic and steel pallets
- Variable speed drive options
- Low maintenance and reliable operation
- Modular design for future expansion
- Designed for continuous-duty applications
System Options
Our pallet handling conveyors can be integrated with a wide range of automation equipment, including:
- Chain transfer units
- Pallet transfers (90° transfer systems)
- Turntables
- Lift stations
- Pallet stackers and destackers
- Pallet dispensers
- Accumulation zones
- Stops and escapements
- Pneumatic or electric pushers
- Barcode scanners and RFID systems
- Weighing stations
- Stretch wrapping machines
- Automatic pallet labelling
- PLC control systems and HMI touchscreens
Whether you’re transporting pallets between production lines, feeding robotic cells, or creating a fully automated warehouse system, Convey Systems delivers reliable pallet handling solutions designed to maximise efficiency, improve safety and reduce operating costs.


Conveyor Turntables
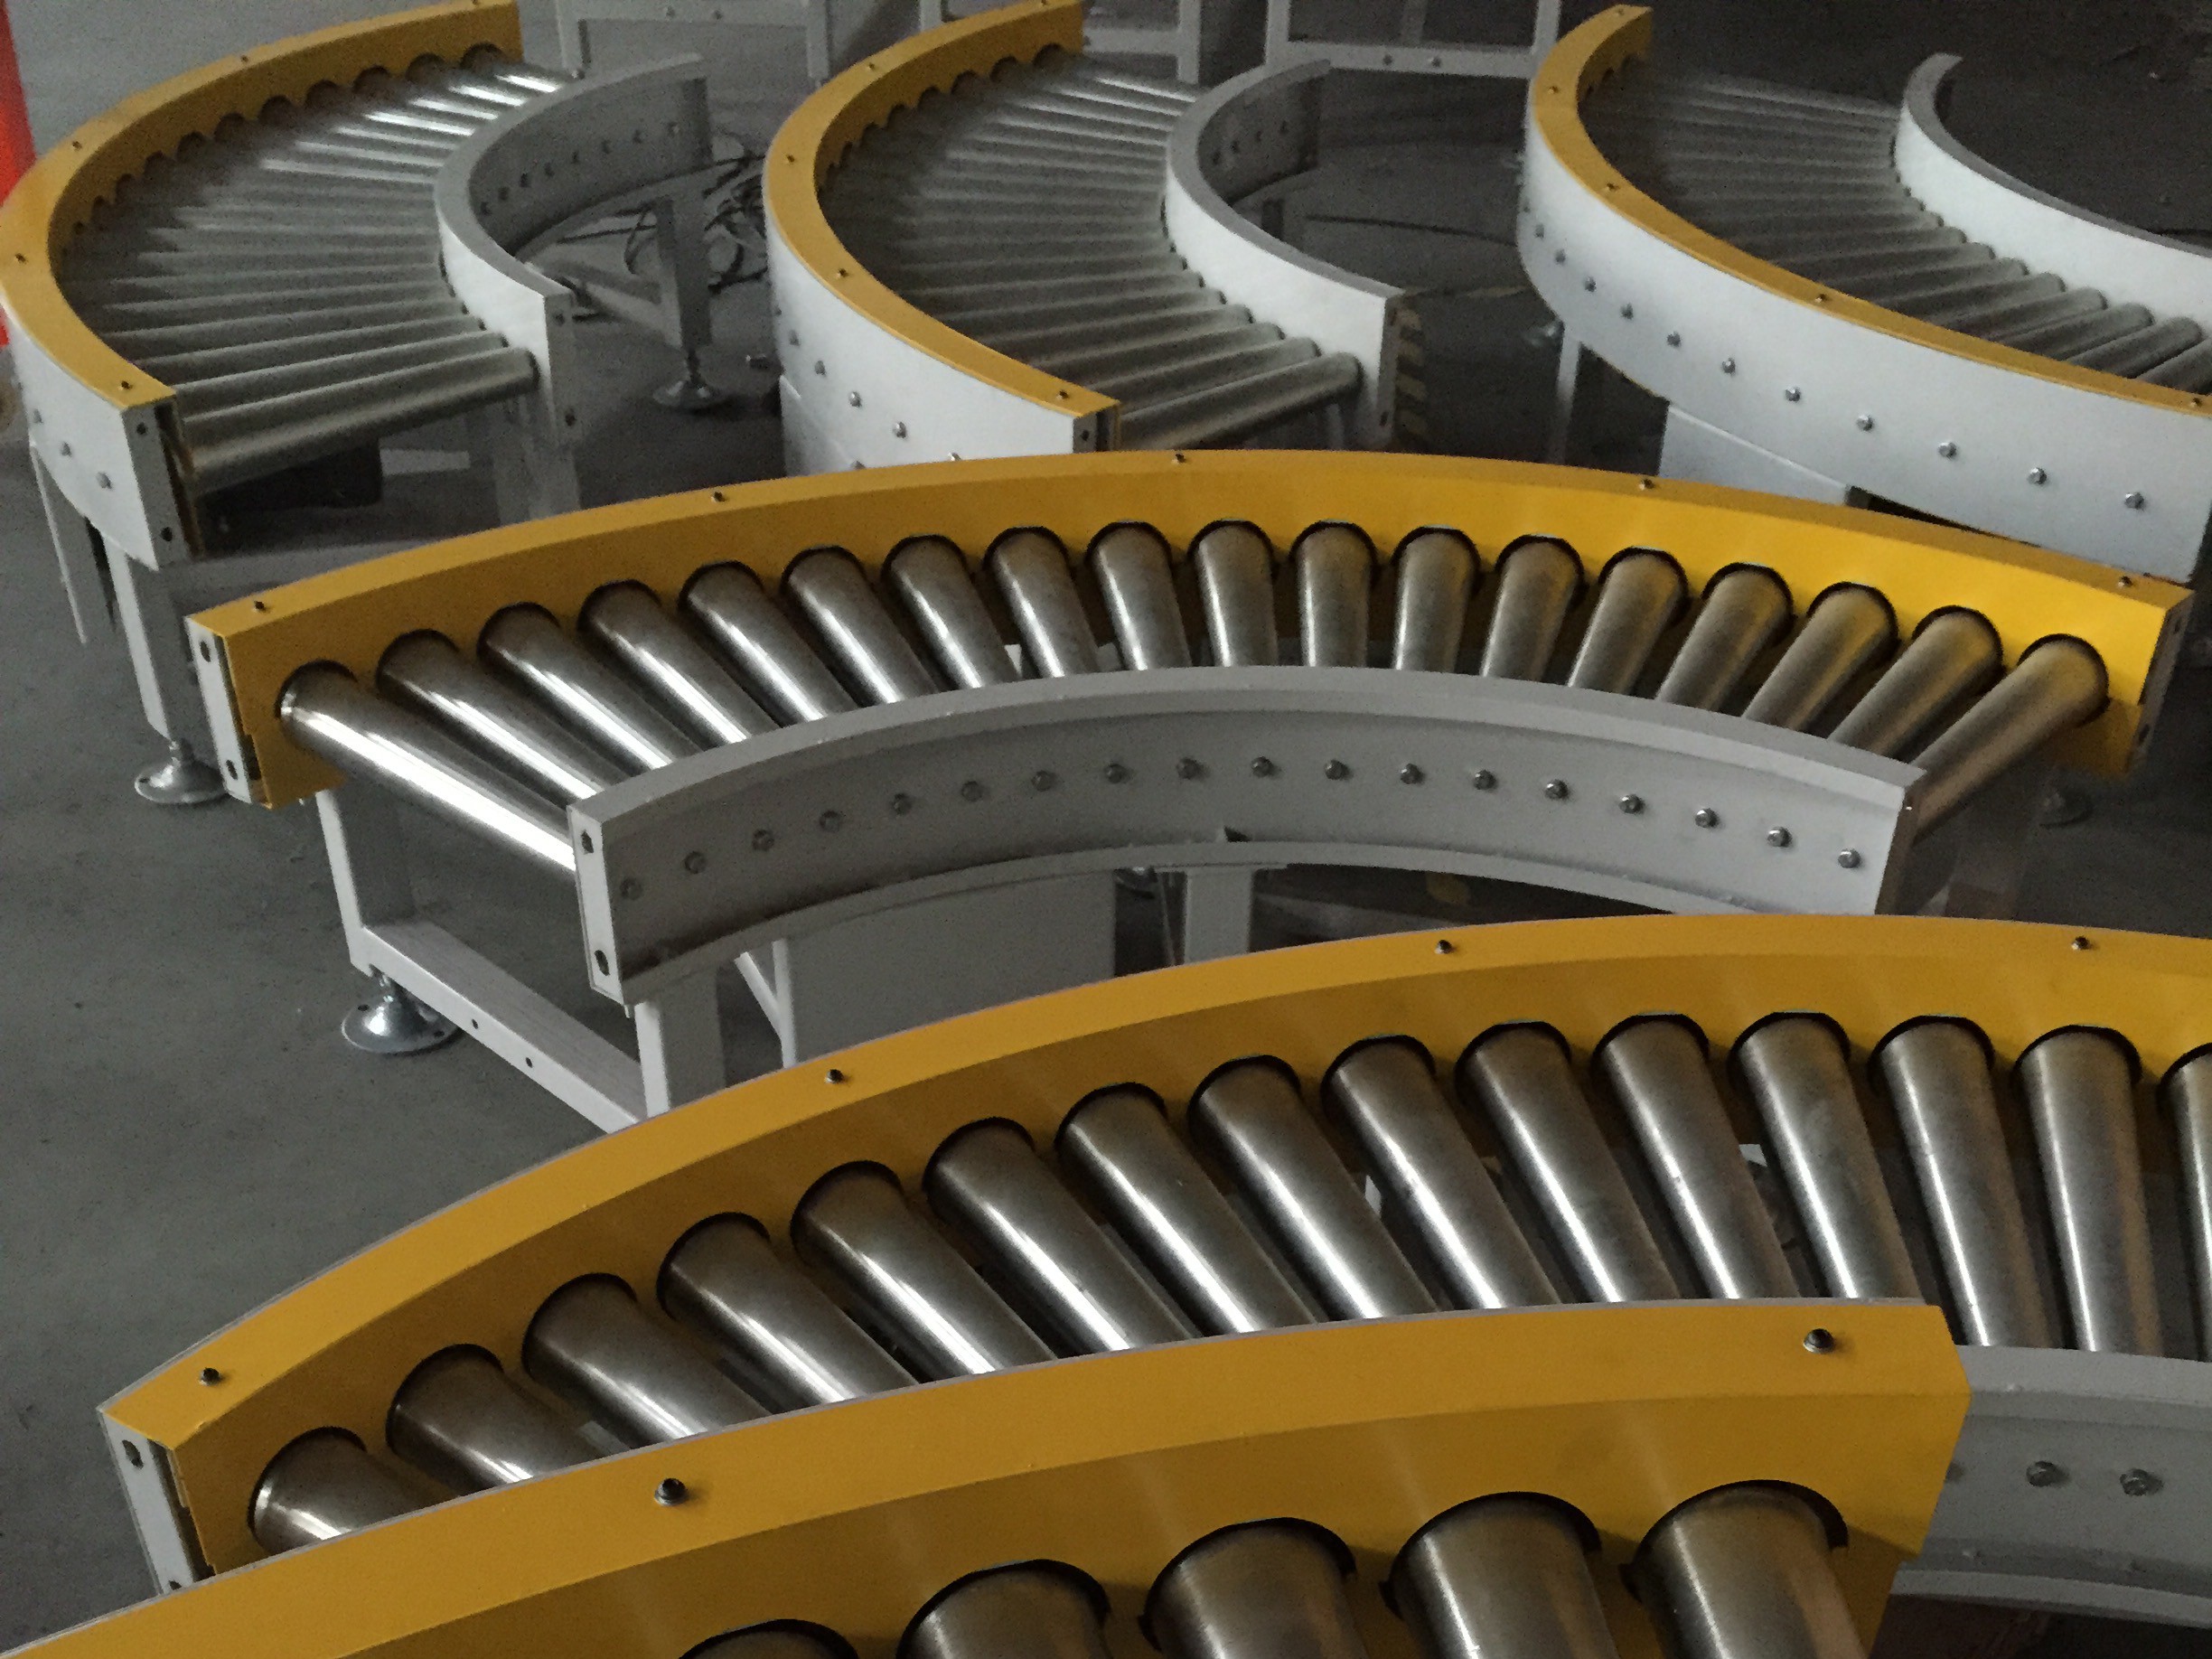
Convey Systems designs and manufactures heavy-duty conveyor turntables that provide a simple and efficient method of changing product direction within conveyor systems. Turntables are commonly used where space is limited or where products need to be rotated or diverted without manual handling, improving productivity while maintaining a smooth flow of materials throughout the production process.
Our conveyor turntables are custom manufactured to suit your application and can be supplied with belt, gravity roller or powered roller conveyor sections depending on your product and system requirements. Available in manual, powered or fully automated configurations, they can rotate products through 90°, 180°, 270° or 360°, making them suitable for virtually any conveyor layout.
Conveyor turntables are widely used throughout the manufacturing, warehousing, logistics, food processing, packaging and pallet handling industries. They provide an efficient solution for changing product direction, transferring products between conveyor lines, feeding multiple production stations and optimising factory floor space.
Our turntables can handle a wide variety of products including:
- Pallets
- Cartons and boxes
- Plastic totes
- Crates
- Drums
- Bags and sacks
- Bottles and containers
- Packaged goods
- Trays
- Industrial components
- Steel products
- Timber products
Every turntable is designed to integrate seamlessly into new or existing conveyor systems and can be supplied as part of a complete automated material handling solution.
Features
Our conveyor turntables are available with:
- Powered roller, gravity roller or belt conveyor surfaces
- Heavy-duty steel construction
- Precision slewing ring or centre pivot design
- Electric geared motor drive
- Variable speed control
- Clockwise and anti-clockwise rotation
- 90°, 180°, 270° or continuous 360° rotation
- PLC and HMI integration
- Photoelectric sensors and automatic positioning
- Emergency stop and safety guarding
- Powder-coated, galvanised or stainless steel construction
- Food-grade designs available
Applications
Conveyor turntables are commonly used for:
- Changing product direction between conveyor lines
- Pallet transfer systems
- Warehouse and distribution centres
- Automated sorting lines
- Packaging and dispatch areas
- Manufacturing and assembly lines
- Food and beverage production
- Bottling and filling plants
- Courier and parcel sorting facilities
- Robotic pick-and-place systems
- Machine feeding and product accumulation
Whether you require a simple pallet turntable, a powered roller turntable for an automated warehouse or a fully integrated product rotation system for a manufacturing line, Convey Systems can design and manufacture a custom solution to suit your exact application. Every turntable is engineered for reliable, long-term performance while improving product flow, reducing manual handling and maximising the efficiency of your conveyor system.


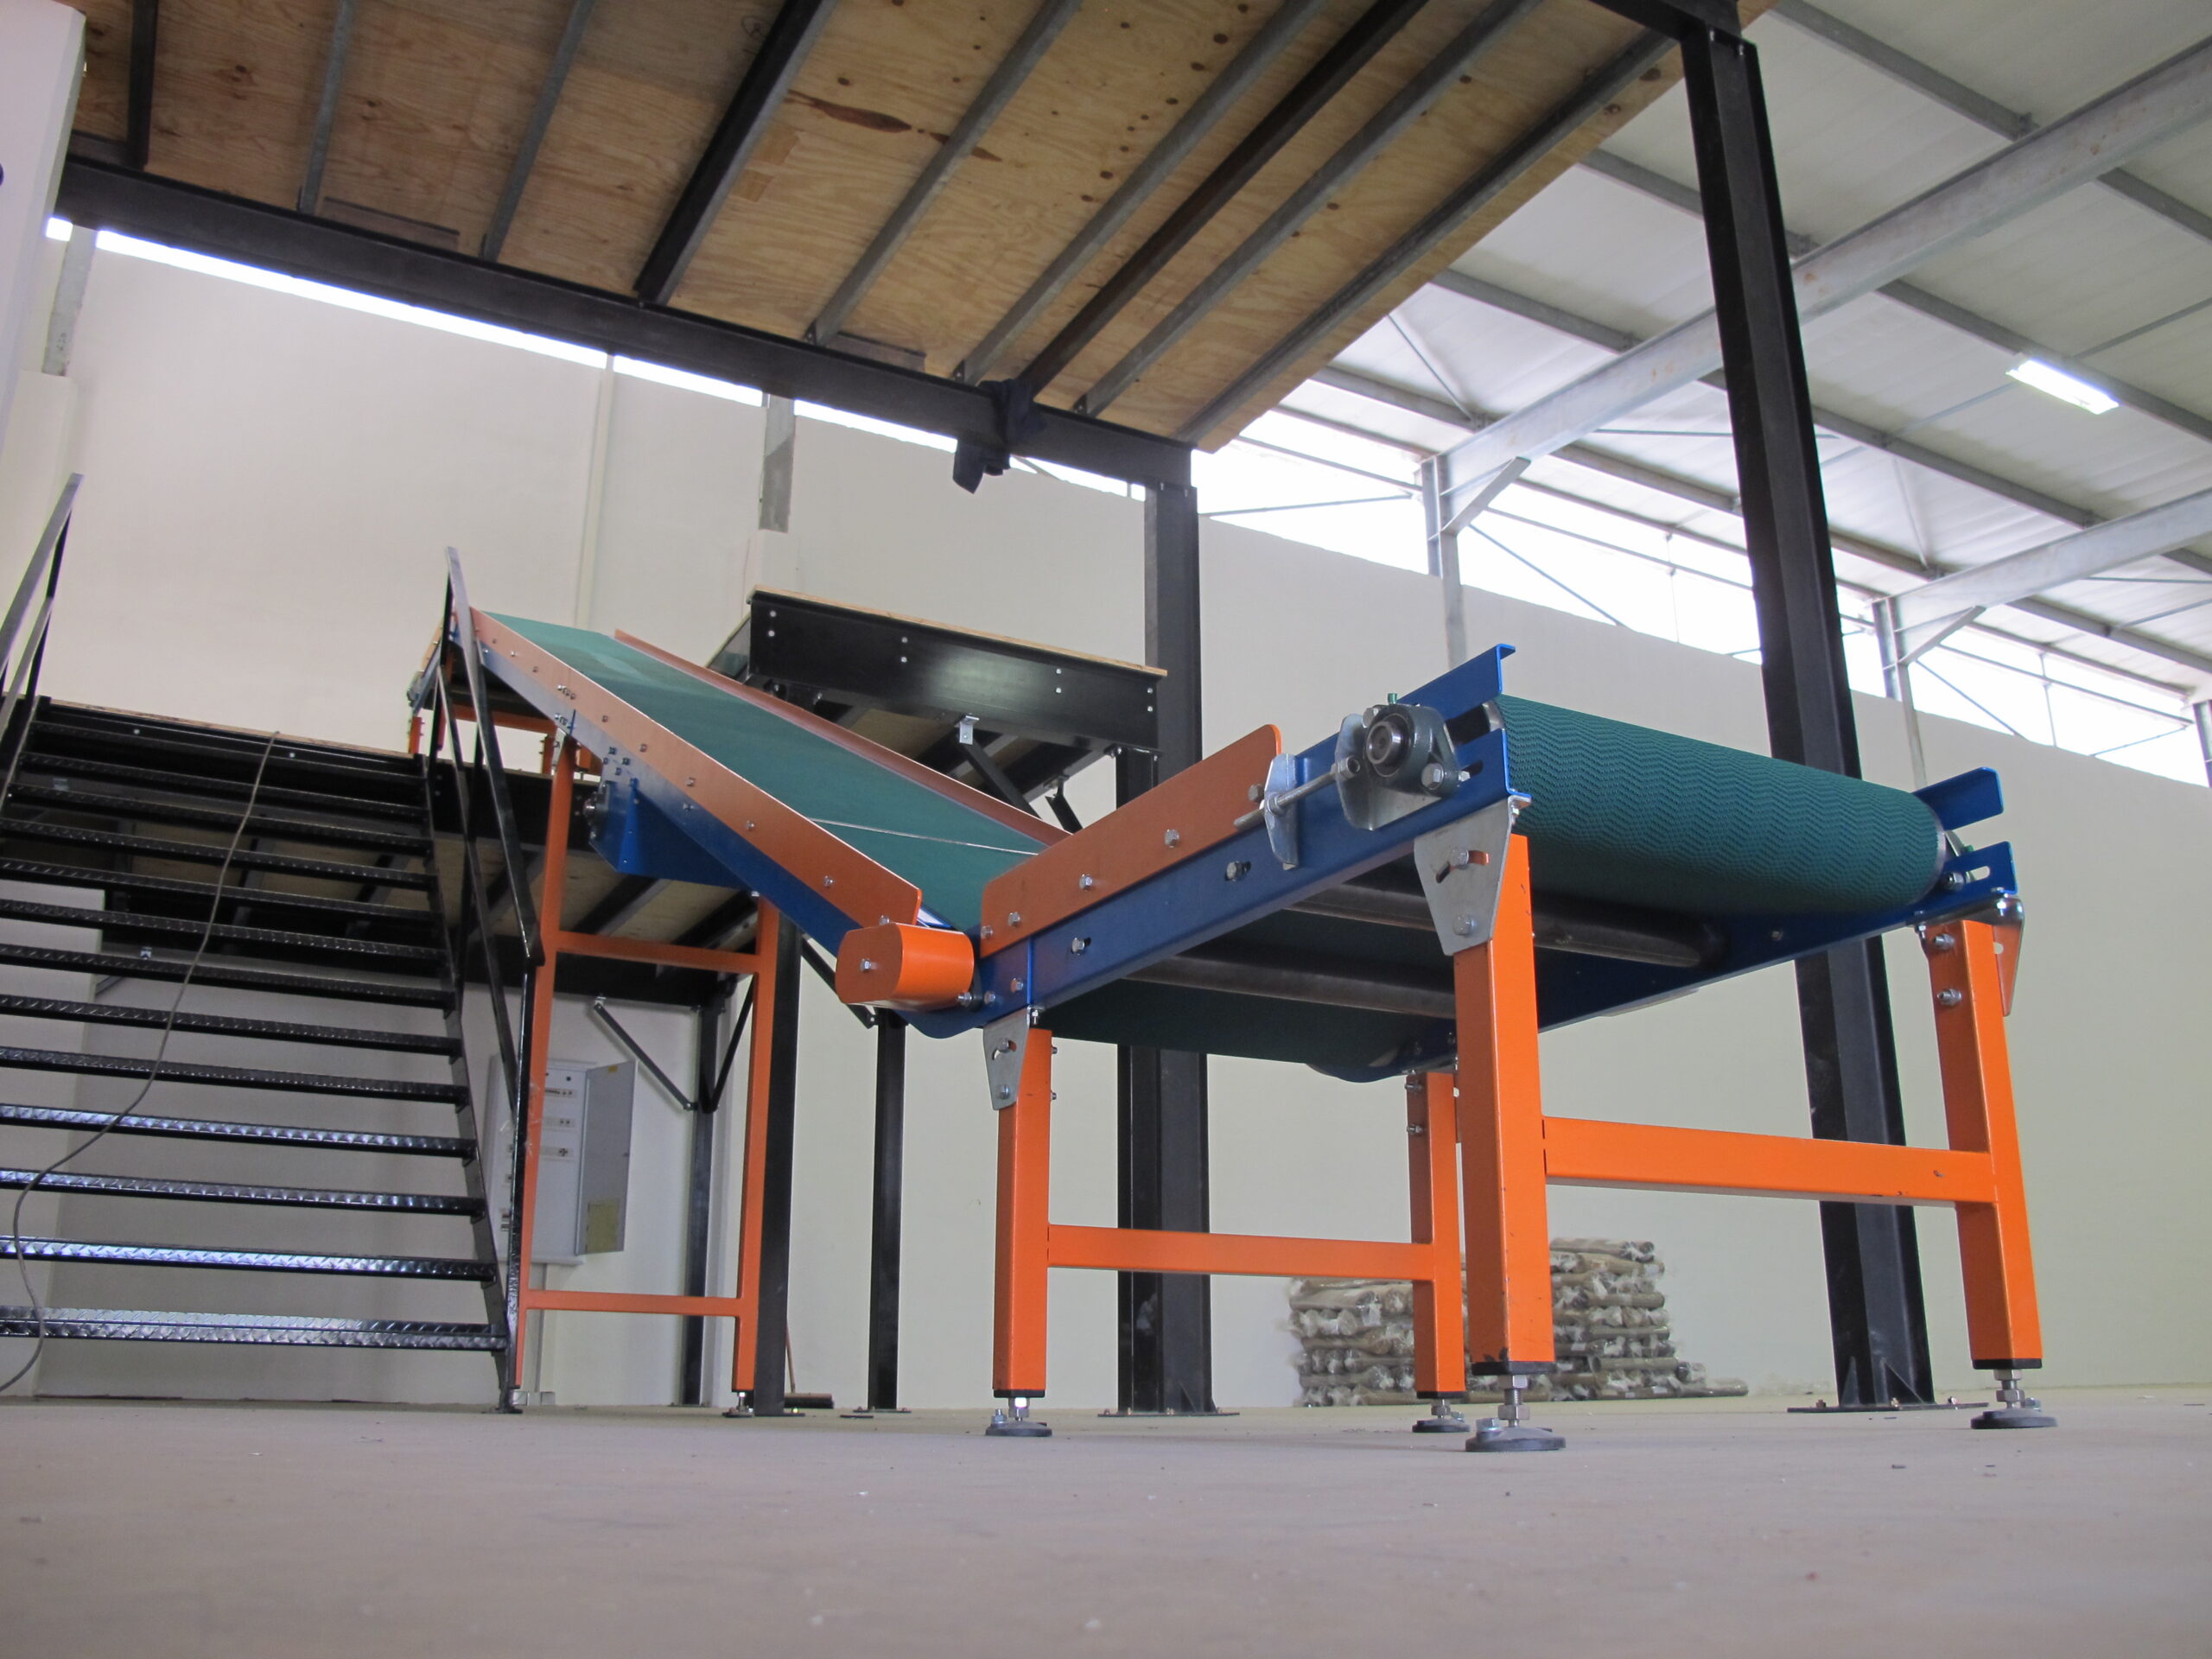
Belt Conveyors
Belt conveyors are one of the most versatile and efficient material handling solutions available. Designed to transport a wide variety of products safely and efficiently, they are suitable for everything from light-duty packages to heavy bulk materials across almost every industry.
At Convey Systems, every belt conveyor is custom designed and manufactured to meet your specific application, ensuring maximum reliability, efficiency and long service life. Whether you require a straight conveyor, inclined conveyor, decline conveyor or a fully integrated conveyor system, we can provide a solution tailored to your operation.
Our belt conveyors are available in a wide range of belt types and frame configurations to suit different products, environments and industries. We supply conveyors for applications including:
- Manufacturing
- Warehousing and Distribution
- Food Processing
- Agriculture
- Mining and Quarrying
- Packaging and Assembly
- Recycling
- Logistics
Features
- Custom-built to your exact requirements
- Heavy-duty steel or stainless steel construction
- Variable speed drive options
- Horizontal, inclined and declined configurations
- Low maintenance and reliable operation
- Energy-efficient drive systems
- Suitable for continuous operation
Belt Options
We offer a comprehensive range of conveyor belts, including:
- PVC Belts
- Food Grade Belts
- Grip Top Belts
- Chevron Belts
- Modular Plastic Belts
- Heat Resistant Belts
- Oil Resistant Belts
- Anti-Static Belts
Our experienced engineering team will recommend the most suitable belt type, drive system and conveyor design based on your product, throughput and operating environment.
Whether you need to move cartons, bags, boxes, components or bulk materials, Convey Systems delivers high-quality belt conveyors engineered for performance, reliability and years of dependable service.


Extruded Aluminium Conveyors
Extruded aluminium conveyors offer a modern, modular and highly versatile material handling solution. Their lightweight yet robust construction allows for rapid assembly, easy modification and exceptional flexibility, making them ideal for fast-paced manufacturing, packaging and food processing environments.
Unlike painted or powder-coated steel conveyors, aluminium conveyors feature a clean, corrosion-resistant finish that requires no painting or surface treatment. Their hygienic design also makes them an excellent choice for food-grade and clean-room applications.
Built using a modular aluminium profile system, these conveyors can be quickly expanded or reconfigured as your production requirements change. Additional equipment can be easily integrated without extensive fabrication, reducing installation time and future modification costs.
Features
- Fast assembly and installation
- Fully modular design for future expansion
- Food-grade and hygienic construction
- No painting or powder coating required
- Lightweight yet extremely strong
- Corrosion-resistant aluminium frame
- Low maintenance and easy to clean
- Custom-built to suit your application
Easily Integrates With
Our extruded aluminium conveyor systems can be supplied with or upgraded to include:
- Workstations
- Packing and assembly tables
- Weighing scales
- Heat tunnels
- Sensors and product detection
- Vision inspection systems
- Barcode scanners
- Label applicators
- Inkjet printers
- Side guides and product stops
- Control panels and automation
- Adjustable support stands
Whether you require a standalone conveyor or a complete automated production line, Convey Systems can design and manufacture a modular aluminium conveyor system that grows with your business while delivering reliable, efficient performance for years to come.


Inter-Floor Belt Conveyors
Inter-floor belt conveyors provide an efficient and reliable solution for transporting products safely between different floor levels within factories, warehouses and distribution centres. Designed to maximize floor space and improve workflow, these conveyors eliminate the need for manual handling while increasing productivity and reducing operating costs.
At Convey Systems, every inter-floor conveyor is custom designed and manufactured to suit your building layout, product type and throughput requirements. Whether you need to transport cartons, crates, bags, boxes or packaged goods, we can engineer a system that integrates seamlessly into your operation.
Our inter-floor conveyors are available in a range of lift heights, with standard designs accommodating floor-to-floor heights from 3,200 mm up to 6,000 mm, while taller systems can be designed to suit specific applications.
Features
- Custom-built to suit your building and application
- Standard floor heights from 3,200 mm to 6,000 mm
- Heavy-duty steel construction
- Continuous-duty drive systems
- Variable speed options available
- Low maintenance and reliable operation
- Custom belt options to suit your product
- Designed for safe and efficient product transfer
Complete Material Handling Solution
To ensure smooth product flow, our inter-floor conveyors can be supplied with:
- Infeed conveyors to feed products onto the incline
- Outfeed conveyors for smooth product discharge
- Accumulation conveyor sections
- Side guides and product tracking
- Adjustable support structures
- Safety guarding and emergency stop systems
- Control panels with PLC automation
- Sensors, photo eyes and product counting
- Integration with existing conveyor systems
Every system is engineered to maximize efficiency while ensuring reliable product handling between floors. Whether you require a simple floor-to-floor conveyor or a fully automated transfer system, Convey Systems can provide a turnkey solution designed specifically for your facility.


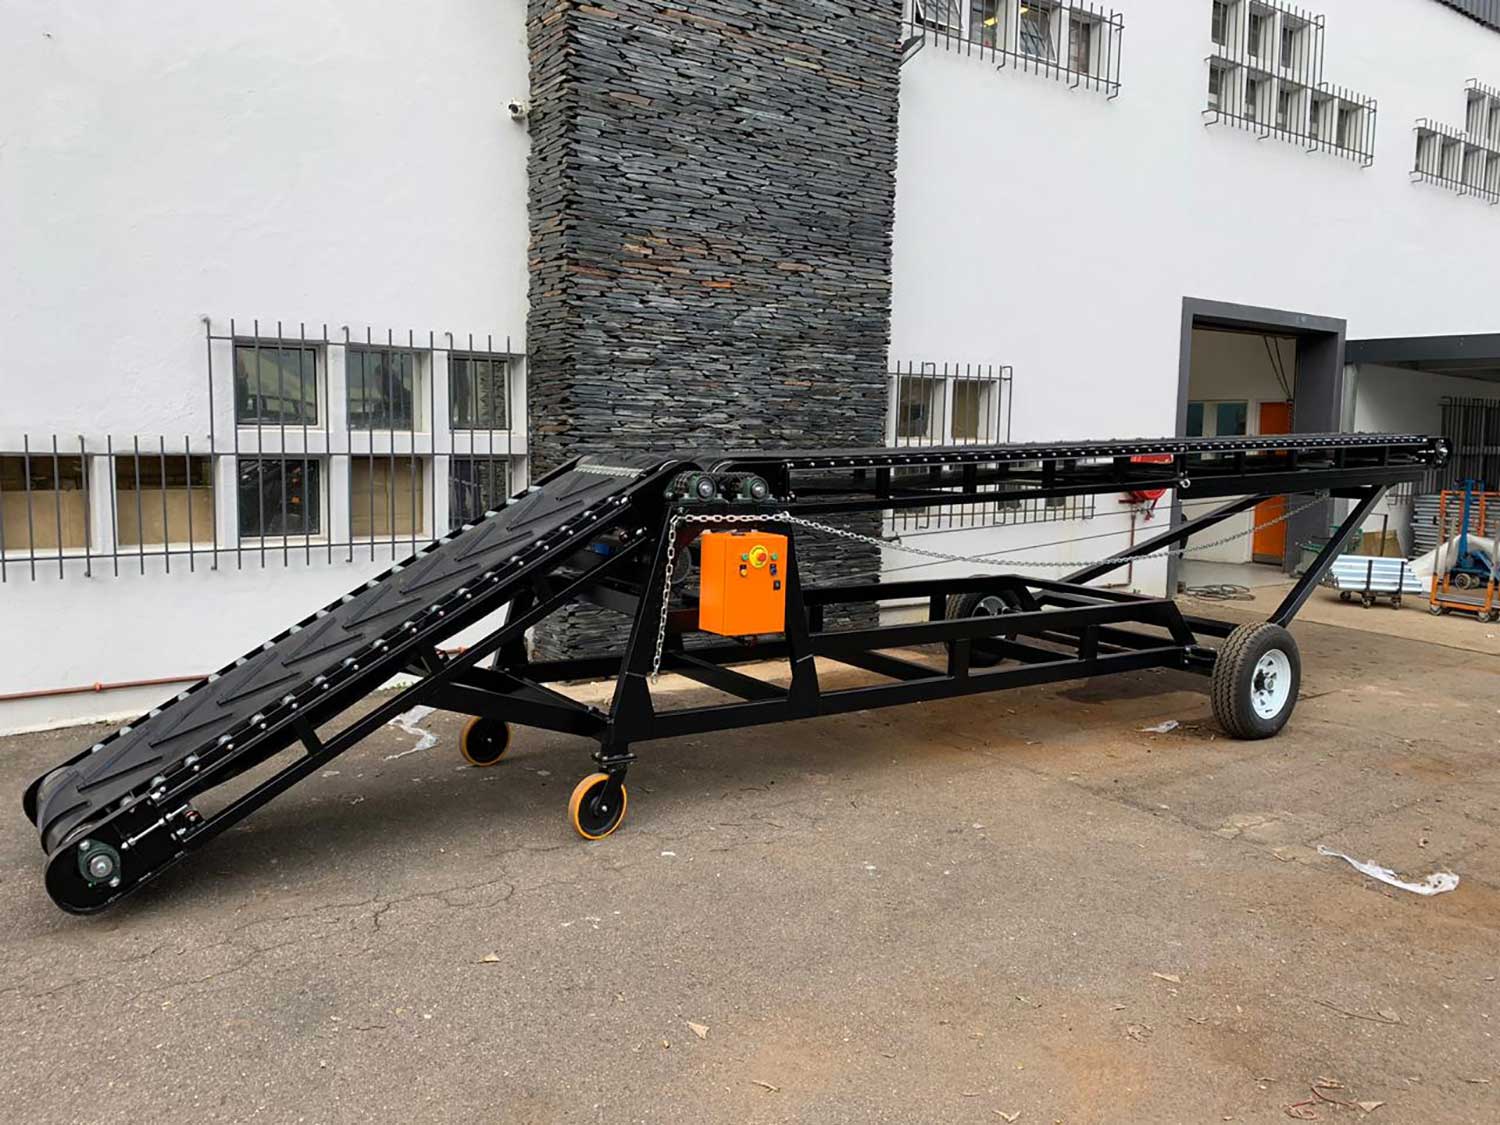
Builders & Construction Conveyors
Builders and construction conveyors provide a fast, safe and cost-effective solution for transporting construction materials around building sites. Designed to reduce manual handling and improve productivity, these conveyors are ideal for moving heavy materials to elevated work areas, scaffolding, upper floors and rooftops.
Built to withstand demanding site conditions, Convey Systems’ construction conveyors feature a robust steel frame, heavy-duty conveyor belt and reliable petrol or diesel drive system, making them suitable for continuous operation on construction sites across South Africa.
Our conveyors are widely used by building contractors, civil engineering companies, brick manufacturers and construction firms for efficiently transporting a variety of materials.
Common Applications
Our builders’ conveyors are ideal for conveying:
- Bricks
- Cement bags
- Concrete
- Wet and dry mortar
- Building sand
- Stone and aggregate
- Blocks
- Roof tiles
- Paving bricks
- Rubble
- Gravel
- Crushed stone
- Topsoil
- Fertiliser
- Firewood
- Landscaping materials
- General building materials
These conveyors are commonly used for:
- Residential construction
- Commercial building projects
- Industrial developments
- Renovations
- Roofing projects
- Civil engineering works
- Landscaping
- Warehouse construction
- Factory maintenance
Standard Specifications
- Available Lengths: 7 m, 10 m, 13 m and 16 m
- Frame Construction: Heavy-duty 38 mm square steel tube
- Capacity: Up to 10 tonnes per hour
- Conveyor Belt: Heavy-duty rubber conveyor belt
- Maximum Incline: Approximately 22°
- Drive Options: Honda petrol engine or diesel engine
- Construction: Heavy-duty design for demanding site conditions
Features
- Fast installation and easy relocation around site
- Heavy-duty construction for long service life
- High-capacity material handling
- Suitable for indoor and outdoor applications
- Reliable Honda petrol or diesel power options
- Minimal maintenance requirements
- Improves site productivity and reduces labour costs
- Safer alternative to manual lifting and carrying
- Custom options available to suit specific site requirements
Whether you’re conveying bricks, concrete, mortar, sand, stone or other construction materials, Convey Systems’ builders’ conveyors provide a reliable and efficient material handling solution that saves time, reduces labour and keeps your project moving efficiently.


Truck Loading Conveyors
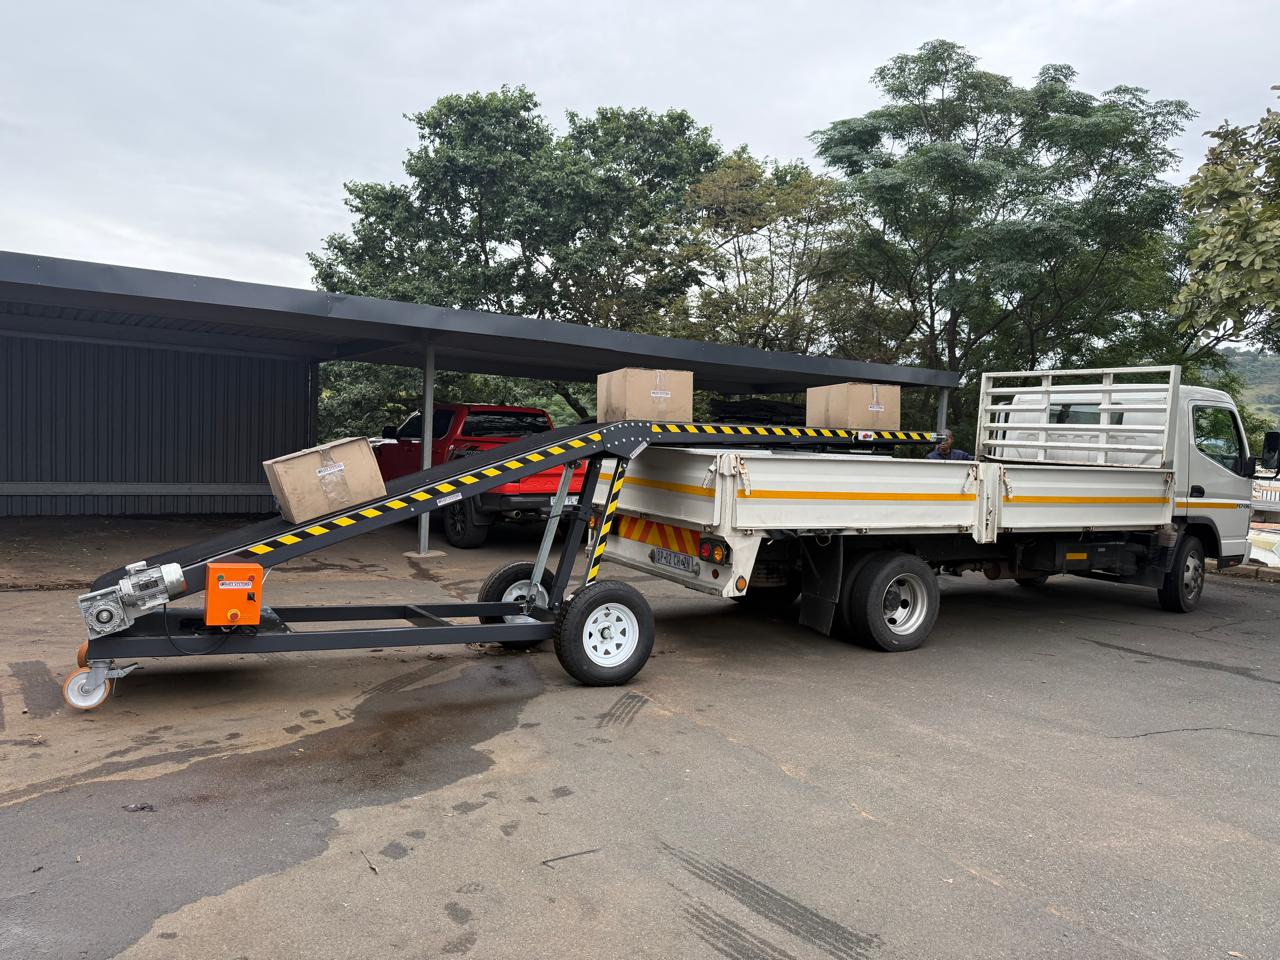
Convey Systems’ truck loading conveyors are designed to speed up the loading and unloading of trucks, trailers and shipping containers while reducing manual handling and improving workplace safety. Built for reliability, mobility and ease of operation, these conveyors are the ideal solution for warehouses, distribution centres, factories, agricultural facilities and logistics operations.
Whether you’re loading cartons, boxes, bags or packaged products, our truck loading conveyors help reduce loading times, minimise labour requirements and increase productivity. Their portable design allows a single conveyor to be easily moved between loading bays, making them a cost-effective solution for busy dispatch and receiving departments.
Manufactured from a robust heavy-duty steel frame with a durable powder-coated finish, each conveyor is designed for continuous industrial use. The adjustable boom height allows operators to position the conveyor at different truck or container heights, while the reversible belt enables both loading and unloading using the same machine.
Standard Specifications
- Boom Lengths: 3.0 m and 4.5 m
- Belt Widths: 300 mm or 600 mm
- Drive: Single-phase electric motor
- Belt Direction: Forward and reverse operation
- Speed Control: Variable speed drive
- Height Adjustment: Hydraulic or manual adjustment available
- Construction: Heavy-duty powder-coated steel frame
- Load Capacity: Suitable for cartons and packages from 10 kg to 30 kg
Features
- Portable design with heavy-duty wheels and swivel castors
- Adjustable boom height and conveyor angle
- Reversible belt for loading and unloading
- Variable speed control for different products
- Rugged steel construction for long service life
- Easy to position and relocate between loading bays
- Low maintenance and reliable operation
- Custom sizes and configurations available
Truck loading conveyors are widely used in warehousing, logistics, courier depots, e-commerce fulfilment centres, agriculture, manufacturing and distribution facilities. They are ideal for loading and unloading cartons, boxes, bags, parcels, packaged goods, seed, fertiliser, animal feed, consumer products and other lightweight to medium-weight items.
Whether you’re loading a delivery vehicle, unloading a shipping container or improving dispatch efficiency, Convey Systems’ truck loading conveyors provide a reliable, portable and cost-effective material handling solution that increases productivity while reducing manual labour and operator fatigue.


Single Boom Stacker Conveyors
Convey Systems’ Single Boom Stacker Conveyors are designed to stack, load and unload bags, boxes and bulk packaged products quickly, safely and efficiently. Their portable, adjustable design makes them ideal for warehouses, factories, agricultural facilities and distribution centres where products need to be stacked at varying heights or loaded directly into trucks and containers.
Built for durability and ease of use, our stacker conveyors reduce manual lifting, improve workplace safety and significantly increase loading and stacking productivity. Whether you’re handling fertiliser, grain, cement, sugar, flour, seed or packaged consumer goods, our stackers provide a reliable material handling solution built to perform in demanding environments.
Manufactured from a heavy-duty steel frame and fitted with a reinforced conveyor belt, every stacker is engineered for continuous industrial use. The adjustable boom allows operators to accurately position the conveyor at the required stacking height, while the portable wheeled design makes it easy to move between workstations.
Applications
Our Single Boom Stacker Conveyors are widely used for:
- Loading and unloading trucks and trailers
- Stacking fertiliser bags
- Handling grain, maize and seed bags
- Sugar and flour bag handling
- Cement and building material handling
- Animal feed and agricultural products
- Warehousing and distribution
- Manufacturing and production facilities
- Packaging and dispatch operations
Standard Specifications
- Available Belt Widths: 600 mm and 800 mm
- Standard Lengths: 10 m and 13 m
- Construction: Heavy-duty steel frame
- Conveyor Belt: Reinforced heavy-duty rubber belt
- Drive: Electric geared motor
- Capacity: Suitable for bags, cartons and products up to 30 kg
- Operation: Forward or reversible belt options available
- Mobility: Heavy-duty wheels with swivel castors
Features
The adjustable boom can be raised or lowered using either a manual or hydraulic height adjustment system, allowing operators to align the conveyor with different truck heights, stacking levels or production equipment. Its rugged steel construction provides excellent durability for continuous industrial use, while the reinforced belt ensures smooth, reliable product handling.
The conveyor’s bi-directional operation allows the same machine to be used for both loading and unloading, providing greater flexibility across multiple applications. Heavy-duty wheels and swivel castors make the conveyor easy to relocate, allowing one unit to service multiple loading bays or production areas.
Whether you’re stacking fertiliser bags in a warehouse, loading seed into trucks, transporting cement bags on a construction site or handling packaged products in a manufacturing plant, Convey Systems’ Single Boom Stacker Conveyors deliver a reliable, efficient and cost-effective material handling solution designed to increase productivity and reduce manual labour.


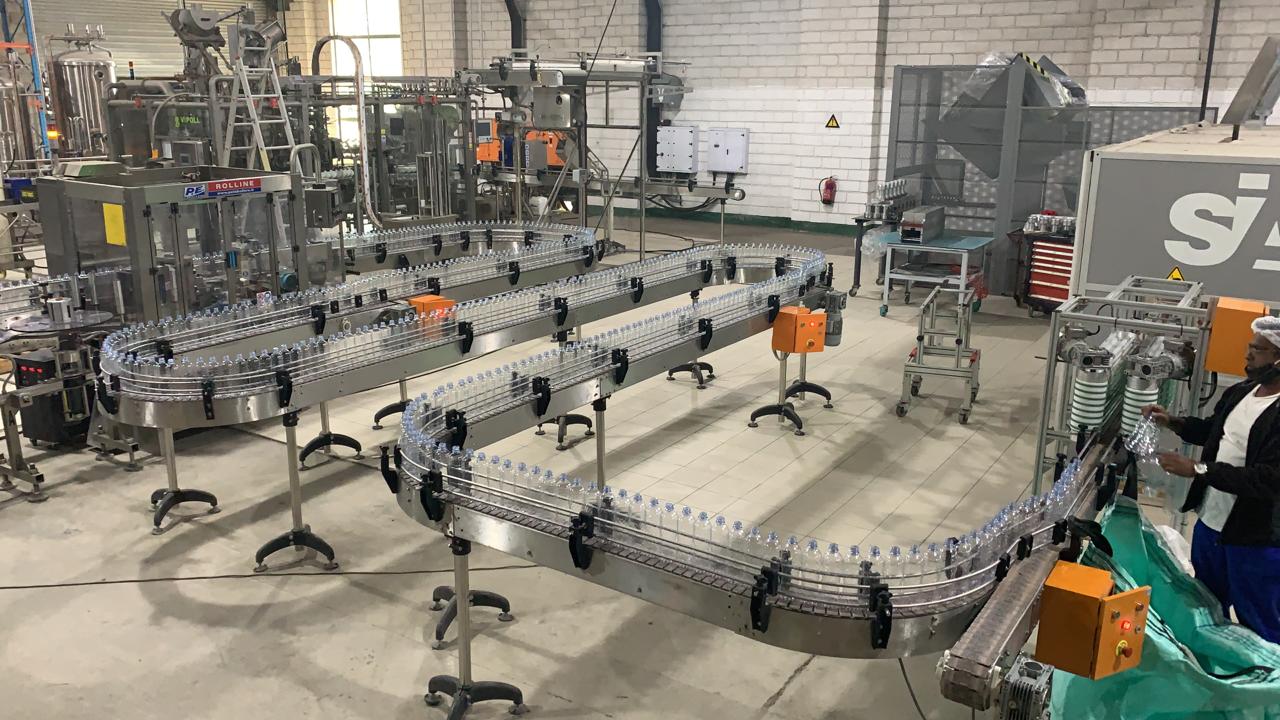
Bottling & Slat Band Conveyors
Bottling and slat band conveyors are specifically designed for the smooth, controlled handling of bottles, cans, jars and other containers throughout filling, labelling, packaging and production lines. Their durable, low-friction design provides reliable product transport while maintaining product stability, even at high production speeds.
At Convey Systems, we design and manufacture custom slat band conveyor systems to suit your production process, available in a variety of widths, lengths and configurations. Whether you require a single conveyor or a fully integrated bottling line, our systems are built for maximum reliability, hygiene and efficiency.
Our conveyors are suitable for industries including beverage, food processing, pharmaceuticals, cosmetics, household chemicals and packaging.
Features
- Custom-designed to suit your production line
- High-speed, continuous product handling
- Food-grade conveyor components available
- Stainless steel or powder-coated steel construction
- Straight, inclined and curved conveyor sections
- Modular design for easy expansion
- Low maintenance and long service life
- Variable speed drive options
System Options
Our bottling and slat band conveyor systems can be integrated with a wide range of production equipment, including:
- Filling machines
- Capping machines
- Labelling machines
- Date coding and inkjet printers
- Bottle rinsers
- Heat tunnels and shrink wrapping equipment
- Accumulation tables
- Rotary tables
- Product guides and lane dividers
- Vision inspection systems
- Bottle reject systems
- Sensors and product counting
- PLC control systems and automation
Available with a wide selection of modular plastic slat chains to suit different container sizes, weights and operating environments, our conveyors provide smooth product transfer while reducing jams and product damage.
Whether you’re installing a new bottling line or upgrading an existing production facility, Convey Systems can deliver a complete conveyor solution designed to maximise efficiency, improve throughput and ensure reliable operation for years to come.


Lift Tables


Roller Tracks


Parts and Accessories


Turnkey Conveyor & Material Handling Projects
At Convey Systems, we don’t just manufacture conveyors—we deliver complete turnkey material handling solutions. From the initial concept through to commissioning and ongoing maintenance, we manage every stage of your project, providing a single point of responsibility and ensuring your system performs exactly as intended.
Our experienced engineering team works closely with every client to understand their production requirements, available floor space, product flow and future expansion plans. Using the latest design software and proven engineering practices, we develop efficient material handling systems that increase productivity, reduce labour costs and maximise operational efficiency.
Whether you require a single conveyor or a fully automated production line, Convey Systems has the expertise to design, manufacture, install and support complete conveyor systems throughout Southern Africa.
Our Turnkey Process
Every project follows a structured process to ensure the highest quality and reliability:
- Initial consultation and site survey
- Process flow analysis and system optimisation
- Concept development and layout design
- 2D manufacturing drawings and 3D modelling
- Mechanical and electrical design
- Custom manufacturing in our South African factory
- Factory assembly and testing
- Delivery to site
- Professional installation
- Electrical integration and PLC programming
- Commissioning and operator training
- Ongoing servicing, maintenance and technical support
Our relationship with our customers doesn’t end after installation. We provide preventative maintenance, breakdown support, conveyor upgrades, system extensions, refurbishments and replacement equipment to ensure your operation continues to perform at its best for years to come.
Industries We Serve
Convey Systems has successfully completed projects across a wide range of industries, including:
- Warehousing and Distribution
- Logistics and Courier
- Manufacturing
- Automotive
- Food Processing
- Beverage and Bottling
- Fruit and Vegetable Packhouses
- Agriculture
- Grain Handling
- Fertiliser Plants
- Seed Processing
- Animal Feed Manufacturing
- Sugar Mills
- Bakeries
- Pharmaceutical
- Cosmetics
- Packaging
- Plastics
- Recycling and Waste Management
- Mining and Quarrying
- Cement and Construction
- Timber and Wood Processing
- Paper and Printing
- Steel and Engineering
- Chemical Processing
- Airports and Parcel Handling
Complete Material Handling Solutions
Our turnkey projects can incorporate a wide range of equipment, including belt conveyors, roller conveyors, pallet handling systems, gravity conveyors, slat band conveyors, fruit sorting conveyors, truck loading conveyors, inter-floor conveyors, stacker conveyors, conveyor turntables, transfers, accumulation systems, weighing stations, barcode scanners, vision inspection systems, robotic interfaces, PLC automation, control panels and safety systems.
Every system is custom engineered to suit your application, whether your objective is increasing production capacity, reducing labour, improving product flow or automating an entire manufacturing process.
From the first concept drawing through to installation, commissioning, maintenance and future expansions, Convey Systems is your trusted partner for complete conveyor and material handling solutions engineered for performance, reliability and long-term value.


Learn More About South Africa’s Top Conveyor Rollers Suppliers
We are experts in the design and manufacturing of conveyor rollers, belts and systems. Thanks to our unyielding commitment to service excellence, we’ve also grown to become one of the top conveyor rollers suppliers in South Africa, and with good reason.
Our team works constantly to keep our catalogue of products up to date and responsive to our customers ever-evolving needs. Today, we continue to design and supply automation equipment to help our clients cope with the demands of modern industry. As a result, we manufacture complete conveyor systems, from simple gravity roller conveyors to fully-automated PLC controlled lines.
What’s more, we also manufacture and supply components for all conveyors, including articulating feet, precision roller bearings, sprockets and pulleys, among many other products and solutions. Throughout the years, we’ve designed systems that feature stainless steel, mild steel and aluminium quite extensively.
What Other Products Do We as Leading Conveyor Roller Suppliers Provide?
Aside from being one of the top conveyor rollers suppliers in South Africa, we also design and manufacture many other conveyor products and systems. These products include:
- Belt and inter floor conveyors;
- Driven roller and slat band conveyors;
- Modular belt and gravity roller conveyors; and
- Bottling slat conveyors and Chain conveyors, to name only a few.
Customer Service Remains Our Top Focus
The core of our business remains excellent customer care. It’s because of this that we offer the best possible service through the manufacturing of exceptional quality equipment, a 24-hour call out service, and expedited delivery lead times. We are always in search of ways to add even more value to our clients’ operations and businesses.
Throughout the years, we’ve worked with leaders in South Africa industry, including brands ranging from Toyota, Defy, Whirlpool, Mondi and Mr Price, among many other brands that have trusted us with keeping their operations moving forward.
Our team is ready to answer your questions, and to provide you with the professional insights and advice needed to make an informed purchase decision. If you would like to learn more about us, and what we can do for you, feel free to contact us today.